Hey everyone, PE Grinding Mill
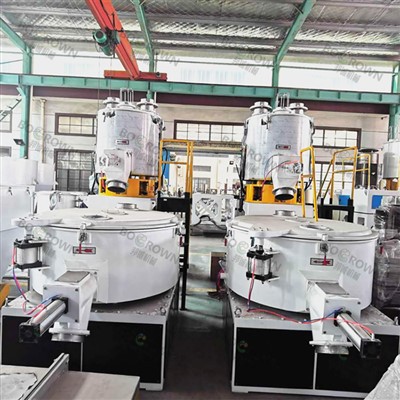
If you’re here, chances are you either run a plastic recycling plant, work in manufacturing that uses ground polyethylene (PE), or maybe you’re just tired of your PE grinding mill eating up your budget without giving you the output you need. Let’s cut to the chase – I’ve been on this side of the industry for years, and I’ve talked to dozens of operators who are struggling with the same issues: inconsistent particle sizes, too much downtime, high energy bills, and that nagging feeling that their mill isn’t working as hard as it should. As a PE grinding mill supplier, I don’t just sell equipment – I help folks actually use it right, because if your mill’s running badly, that’s bad for you and bad for the feedback I get. Today, I’m walking through the real, actionable steps to optimize your PE grinding mill operation – no fancy jargon, just stuff that works.
First up: you can’t optimize what you don’t monitor. I see so many operators hitting “go” and checking in once a day, but grinding mills are dynamic beasts. They change every time the feedstock changes, every time you adjust the blades, even when the power dips a little. What should you track? Let’s keep it simple. First, motor amperage. If your amperage spiking or dropping randomly, that’s a red flag – either your feed is too thick, blades are dull, or there’s something jammed in the chamber. I’ve had customers tell me they ignored amperage spikes for weeks, only to blow a motor that cost them $5k and two days of production. Next, particle size distribution. If all you’re checking is if the material fits through a sieve, you’re missing half the picture – too many fines mean you’re wasting energy grinding smaller than needed, too many oversize pieces mean your next process (like washing or extruding) is going to get clogged. And don’t sleep on downtime – track why your mill stops: is it blade changes? Jams? Screen changes? Last year, a client of mine was shutting down 12 times a shift for screen clogs because he was using the wrong screen mesh for his soft LDPE vs hard HDPE. That’s a fixable issue, not a “this mill is trash” issue.
Now, the feedstock part – this is where most people mess up, and it’s not the mill’s fault. PE comes in so many forms: bottles, film, rigid chunks, lumps with labels or adhesives, even wet material. If you toss any old PE into your mill, you’re setting yourself up for trouble. Let’s break it down. First, sort your feed properly. Mixing soft LDPE film with rigid HDPE chunks? The film will wrap around the rotor blades, causing jams and uneven grinding. Last month, I talked to an operator who was mixing post-consumer PE bags with milk jugs, and his mill was producing 20% oversize material because the soft film wasn’t being ground evenly. Second, prep the feed before it hits the mill. If you have big chunks, use a primary crusher to break them down first – don’t feed 1ft wide bottle chunks into a mill made for 2in pieces. And get rid of contaminants as much as possible: labels, glue, metal bits, even water. Water is a big one – wet PE clumps together, causes screens to blind, and adds unnecessary moisture that messes with downstream processes. We actually recommend a drying step for wet PE before grinding, even if it’s just a 10-minute pass through a low-temp dryer. I know, it’s an extra step, but trust me – it cuts grinding time per pound by 15% for most of our clients.
Next, the mill’s core parts – the blades and the screen. These two are make or break, and most operators don’t pay enough attention to them. Let’s start with the blades. Dull blades aren’t just inefficient – they’re dangerous. When blades are dull, the mill has to work harder to tear through PE, which spikes amperage, increases heat, and wears out other parts faster. How do you know when to replace them? Don’t wait until the mill starts making noise. Check the edge of the blades monthly – if they look rounded or have chips, it’s time to change. And when you do change blades, don’t cheap out. We supply high-chrome blades that last 3x longer than standard steel, but I’ve had clients who bought cheap blades that wore out in 8 hours, vs 24 hours for ours. Also, balance the blades when you replace them – unbalanced blades cause vibration that wears out the rotor and bearings, and that’s a quick way to end up with costly repairs.
Then the screens – the unsung heroes of consistent particle size. The screen’s job is to let ground PE through, but if it’s not the right size or it’s dirty, you get all kinds of issues. First, match the screen mesh to your end product. If you need 5mm ground PE for extrusion, don’t use a 3mm screen – that’s wasting energy grinding smaller than needed. I see this all the time: operators buy a mill with a bunch of extra screens and just use the middle one for everything, which is a huge waste. Second, clean the screens regularly. Blinding (when fine PE particles clog the screen holes) is the #1 cause of inconsistent output. How often? If you’re grinding soft film, maybe every 2 hours; rigid PE, maybe every 4. We recommend adding a small air blast system to your mill – it blows air through the screen during operation, preventing clogs, and that simple add-on boosts output by 10-15% for most operations. Also, replace screens when the holes start to wear out – over time, screen holes get bigger, so you’re getting larger particles than you specified. It’s easy to check: hold a new screen next to the old one, and if the holes are noticeably bigger, swap it.
Now, operational settings – this is where you can tweak things without buying new parts. Let’s talk about rotor speed first. A lot of operators set the rotor speed and forget it, but adjusting it based on feedstock makes a huge difference. For soft LDPE film, a slower rotor speed (around 800-1000 RPM) works better – faster speed will just wrap the film around the blades. For rigid HDPE or polypropylene chunks, a slightly faster speed (1000-1200 RPM) gives better grinding without overworking the blades. I know it’s a small adjustment, but one client I worked with increased his output by 18% just by switching from a fixed speed to a variable speed drive (VSD) – he could adjust speed on the fly for different feedstocks. And VSDs aren’t as expensive as you think, they pay for themselves in 3-6 months from energy savings alone.
Another setting: the gap between the rotor blades and the stator (the fixed blades on the mill chamber). This gap controls how fine the PE gets. If the gap is too big, particles don’t get ground enough, leading to oversize material. If it’s too small, you’re grinding particles smaller than needed, wasting energy and creating unnecessary fines. How do you set it? Most mills have adjustment bolts on the chamber – start with the manufacturer’s recommended setting, then tweak it based on your particle size checks. Once, a client called me complaining about too many fines, and we adjusted the gap by just 0.5mm – his fines dropped by 22% instantly, no other changes needed. That’s the kind of small tweak that adds up to big savings.
Also, don’t forget about safety and maintenance routines that actually work. I see operators skipping small maintenance to save time, which ends up costing them way more. Do daily checks: make sure all bolts are tight, no loose parts, the air blast system is working, screens are clear. Weekly checks: lubricate bearings, inspect blades for chips, clean the mill’s internal chamber (old PE buildup can throw off balance and cause jams). Monthly checks: inspect the motor for wear, test amperage levels, check screen hole size. And when you do maintenance, shut the mill down completely and lock it out – I don’t care if it “just needs a quick check,” safety is non-negotiable, but it also prevents accidents that shut you down for days.
Wait, let’s talk about a common mistake I see all the time: overloading the mill. Operators think “more in = more out,” but that’s not true. If you feed too much PE at once, the mill gets jammed, amperage spikes, and you have to shut down to clear it. The sweet spot is feeding the mill at a rate where the motor is running at 80-90% of its rated amperage – that’s when it’s working hard but not straining. If your amperage is constantly over 95%, you’re overloading, and if it’s under 70%, you’re not using the mill’s capacity. I had a client who was feeding 20% more than his mill’s rated capacity, and he was shutting down for jams 5 times a shift. After adjusting feed rate, he only shuts down once a shift for screen changes, and his energy bill dropped by 12%. That’s a no-brainer.
Now, a few last tips that aren’t just technical – they’re about mindset. If your mill is old, don’t assume it’s the problem. We’ve had clients with 10-year-old mills that are running 30% better just by following these steps. On the flip side, even a brand new mill won’t run well if you’re feeding it garbage or skipping maintenance. And when you’re trying things, take data. Track output per hour, energy use per pound of ground PE, downtime, particle size. If you adjust the gap, note how it changes those numbers – that way, you’ll know what works for your specific operation, not just generic advice.
At the end of the day, optimizing a PE grinding mill isn’t about buying a $100k upgrade – it’s about paying attention to the little things, using the right feedstock, adjusting settings to match your material, and staying on top of maintenance. As a supplier, I’m here to back that up – we don’t just sell mills, we give you the know-how to run them right. If you’re tired of poor output, high energy costs, or constant downtime, hit us up to talk through your specific operation. We can help you figure out exactly what tweaks you need, no pressure, just real advice from someone who’s in the thick of this industry every day.
Horizontal Plastic Crusher References:
- Plastics Technology, “Optimizing Size Reduction for Polyethylene Recycling,” 2022.
- American Pulverizer Company, “Best Practices for PE Grinding Mill Operation,” 2021.
- International Association of Plastics Recyclers, “Feedstock Preparation for Grinding Operations,” 2023.
- Journal of Material Processing Technology, “Effects of Blade Condition and Screen Mesh on PE Grinding Efficiency,” 2020.
ZJG BC Machinery Co., Ltd.
As one of the most professional pe grinding mill manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy cost-efficient pe grinding mill for sale here from our factory. Contact us for custom service and OEM service.
Address: No.8 Lexi Road, Leyu Town, Zhangjiagang City
E-mail: sales@bcextruder.com
WebSite: https://www.bcextruder.com/
